Tissue Folding Machine Factory Insights for Reliable Production Line Setup
2026-10-06
Setting up a tissue folding line is rarely about the machines alone—it is about the factory floor realities that spec sheets never show. Most guides stop at speed and capacity, but the difference between smooth output and constant downtime often hides in small operational details. DAXIN brings those details to light, sharing practical, floor-tested insights for building a reliable production line from day one.
Reading the Factory Floor Before You Automate
The promise of automation often seduces manufacturers into buying robots before understanding the humans who currently do the work. Walking the floor with a notebook instead of a vendor's catalog reveals bottlenecks that no sensor suite will detect: the undocumented twist a veteran operator gives a misaligned part, the informal visual check that saves a batch from the scrap bin, the way work orders actually flow when the ERP system is down. Mapping these realities first turns a capital expense into a surgical improvement, not a glorified conveyor belt that locks in today's chaos.
Automation built on a faulty reading of the floor compounds variance rather than eliminating it. A cell designed around theoretical cycle times will idle while operators improvise around tool wear or incoming material inconsistencies that never appeared in the simulation. By contrast, spending two weeks watching shift changes, maintenance calls, and the unofficial problem-solving that happens at coffee breaks gives you the true takt time, the real defect sources, and the tribal knowledge that should be encoded into the machine's logic. Without that grounding, you are automating a guess.
The best first step is often the cheapest: chart the physical path of a single part from receiving to shipping, mark every wait and rework loop, then ask the person doing the job what they would change if they never had to touch it again. That answer—not a sales pitch—becomes your automation spec. You will discover that some tasks vanish when you fix a material handling issue upstream, while others demand cobots that augment rather than replace. Reading the floor first means the automation you eventually install is a mirror of how the work actually happens, not how a spreadsheet imagined it.
Where Tissue Folding Lines Drift Out of Spec
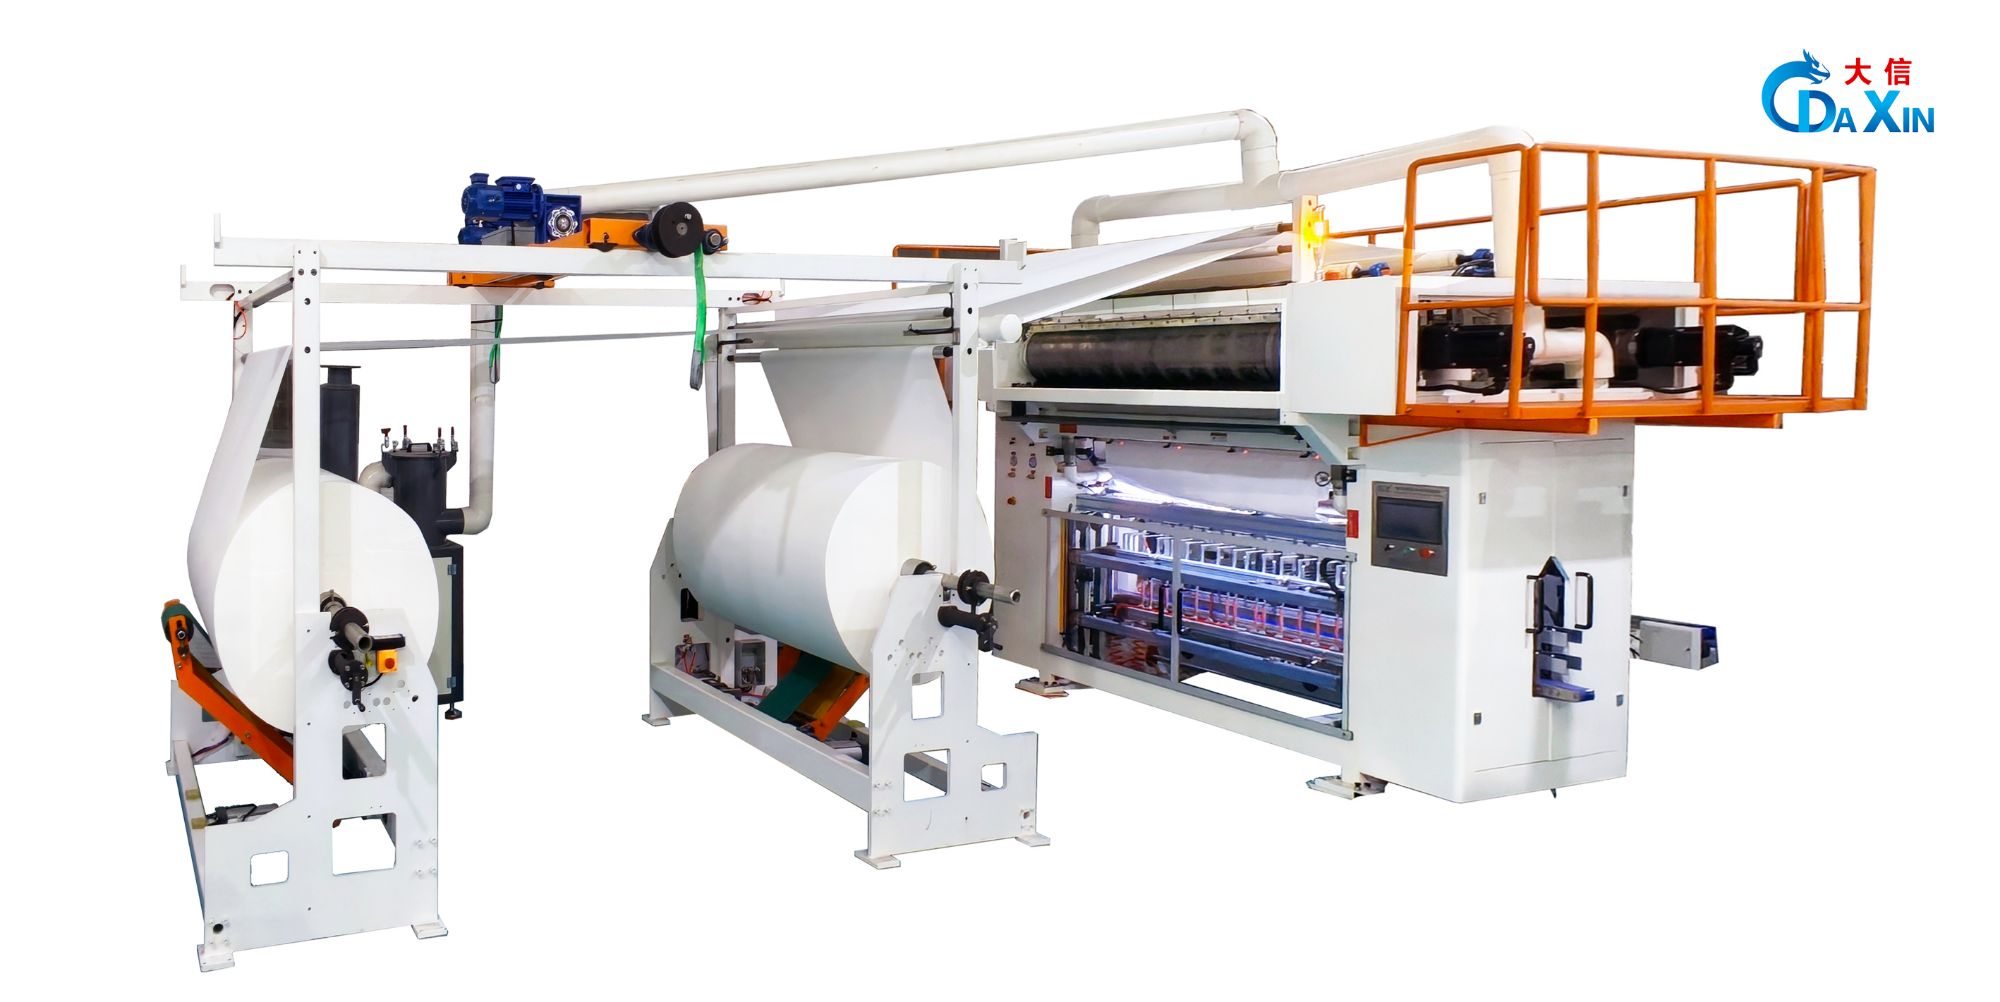
Folding line drift rarely shows up as a sudden jump. More often it starts as a few millimeters of wander that operators catch during a routine check, then it slowly builds into visible misalignment at the packaging or cutting stage. The usual triggers are uneven moisture across the parent roll, slight changes in basis weight from one jumbo to the next, or tension fluctuations as the unwind diameter shrinks. Any of these can push the sheet slightly sideways before the folding plates ever touch it.
On the mechanical side, worn folding roll bearings and guide rolls that are no longer perfectly parallel get overlooked because the problem shows up somewhere else. A tiny angular error in the sheet path can accumulate over dozens of meters and shift the fold line consistently to one edge. Swapping out a folding blade may bring things back in spec for a shift or two, but the drift comes back unless the real source—often a misaligned idler or uneven nip pressure—is corrected.
Tracking the fold position against line speed, unwind tension, and moisture readings helps separate material-related drift from mechanical drift. Many lines rely on manual adjustments at the folding station, but repeated corrections usually mean the root cause is still upstream. In those cases, checking roll surface wear, air cylinder response time, and guide roll alignment tends to reveal why the fold line keeps wandering out of tolerance.
Matching Folder Speed to Real Demand, Not Theory
Most folder gluer spec sheets list a maximum speed that rarely survives contact with a real job. Short runs, awkward board grades, and operator fatigue all chip away at that headline number. What actually matters is how fast the machine can run in your typical mix of orders, not on a test bench.
Take a plant that handles 300 small batches a week. A machine rated at 400 meters per minute sounds impressive, but if each setup takes ten minutes longer than a mid-speed model, the extra top end never gets used. The average speed across a shift ends up lower, and the crew spends more time adjusting than producing. A machine that changes over quickly and holds a steady 180 meters per minute often delivers more finished cartons by Friday afternoon.
A practical way to match speed to demand is to pull six months of production logs. Look at actual running speeds, the number of stops per hour, and the distribution of run lengths. If most orders are under 5,000 sheets, prioritize setup speed and stability over outright velocity. Also factor in board caliper and glue type—some materials simply won't tolerate high-speed folding without cracking. Training operators to handle the machine's sweet spot is just as important as the motor's capability.
Small Adjustments That Keep Changeovers from Eating Your Shift
Even if you can't overhaul the entire setup process, a handful of tiny shifts in how you stage tools, label parts, and sequence tasks can claw back serious minutes. Start by staging everything at the point of use the night before – not just the obvious wrenches and dies, but the less glamorous items like torque specs, purge buckets, and alignment pins. When operators aren't walking back to the crib or hunting for a missing gauge, the clock stops bleeding.
Another overlooked lever is the handoff between roles. Instead of one person doing the full teardown and rebuild, split the changeover into parallel lanes: while the old tooling comes out, someone else preps the new material and double-checks the first-off checklist. It's a small rethinking of who does what, but it turns a serial bottleneck into overlapping work – and that's often enough to keep a thirty-minute changeover from quietly becoming fifty.
What Maintenance Logs Reveal Before a Line Stops
Scattered across maintenance logs are the faint fingerprints of an impending shutdown: a vibration reading nudged above baseline, a temperature curve flattening when it should climb, a note scrawled in the margin about a sound that wasn't there last week. These entries rarely announce themselves as warnings. They read like routine housekeeping—minor adjustments, brief inspections, a seal replaced before its time. Yet when lined up chronologically, they form a quiet countdown. The log doesn't scream; it whispers in decimals and timestamps. Technicians trained to document exactly what they observe, without interpretation, often capture the earliest tremors of failure without realizing it.
The true signal hides not in any single entry but in the drift between them. A pump that ran 48 cycles per hour for three months suddenly logs 46, then 45, then 45 again. No individual record crosses a threshold, no alarm triggers, but the trend is undeniable to anyone who reads the log as a narrative rather than a checklist. Experienced operators learn to spot these subtle shifts—the same way a doctor notices a patient's handwriting getting smaller or a farmer smells rain before the forecast. The logs reveal that breakdowns are seldom abrupt; they are negotiated over days and weeks, with the machine pleading its case in grease samples, amp draws, and filter change intervals.
Ironically, the most valuable entries are often the vaguest. A line that says "checked bearing, seems okay for now" carries more predictive weight than a clean digital readout. It captures hesitation, the human intuition that something is off even when the numbers say otherwise. Maintenance logs, unlike sensor dashboards, preserve doubt. They document the moments when a technician paused, listened, and decided to check again tomorrow. In the days before a line stops, that doubt grows denser, until the final entry reads like a sigh: "will monitor closely next shift." By then, the machine has already told its story. The log simply holds the transcript.
Building a Layout That Survives Operator Turnover
A workstation built around a single skilled operator falls apart the moment that person leaves. Instead, the physical arrangement itself should carry the operational knowledge. Mount shadow boards with exact outlines for each tool, not just labels—new operators can see at a glance what belongs where and notice when something is missing before it causes a defect. Use floor markings and bin positioning that mirror the sequence of work, so the next step is always within arm's reach. This way, the layout acts as a silent trainer, reducing the need for verbal handoffs that get lost between shifts.
Modularity matters more than most managers realize. When a workstation is bolted to the floor and custom-built around an individual's height or reach preferences, every operator change forces a costly rebuild. Design work surfaces, part feeders, and monitor arms to adjust with simple tools—or no tools at all—so a new hire can tweak the setup in minutes without disrupting production. Standardize the connection points and cable routing, leaving enough slack that swapping out a subassembly doesn't require an electrician. The layout should treat the operator as a replaceable component, not a permanent fixture.
Finally, embed constraints that prevent errors rather than relying on operator memory. A chute that only accepts parts in the correct orientation, a fixture that won't clamp unless the workpiece is seated properly, or a sensor that blocks the next cycle until all fasteners are torqued—these physical rules don't disappear when someone quits. Combined with a clear visual flow from raw material to finished goods, the layout enforces the process regardless of who stands in front of it. The goal is a workspace where a competent newcomer can be productive on day one, not after three weeks of tribal knowledge transfer.
FAQ
Pay attention to how the factory organizes its assembly area and whether finished machines undergo a full production cycle test before shipping. A clean, well-documented workflow often indicates that the manufacturer can handle consistent output and after-sales support without cutting corners.
Plan the line layout around material flow rather than just floor space. Keep raw tissue rolls close to the unwinding stations and leave enough clearance for waste bins and operator walkways. Also confirm that the factory provides detailed CAD drawings so your team can simulate daily movement before the machines arrive.
Even the most precise machine will underperform if operators struggle with changeovers or basic troubleshooting. Ask the factory whether they offer on-site training that covers not just button pressing but also cleaning procedures, sensor calibration, and error code interpretation. A short hands-on session during installation can prevent weeks of downtime later.
Request the machine's dimensional drawings, utility requirements, and spare parts list with expected wear intervals. Also ask for a sample of the factory's service reports from previous installations. Documents that show real troubleshooting steps and maintenance logs indicate the manufacturer has dealt with actual field conditions, not just lab tests.
Send a few rolls of your actual tissue to the factory and ask them to run a folding trial while you watch via video or in person. Compare the folded stack height, edge alignment, and jam rate against your current line. Never assume that a machine tuned for soft two-ply bath tissue will perform the same with stiff napkin stock.
Many buyers focus on motor speed but ignore the tension control system and sensor durability under dust buildup. Ask about the recommended cleaning frequency for photoelectric sensors and whether the factory uses sealed bearings on folding rollers. A small dust seal upgrade can save hours of unscheduled stops every month.
Look at the service area and talk to the technicians, not just the sales team. Ask how long it takes to replace a folding plate or a worn timing belt. If the factory keeps these parts in stock and can provide exact replacement time estimates, your maintenance budget will be more realistic. Avoid manufacturers that only show you polished showroom units and avoid questions about wear parts.
Conclusion
A dependable tissue folding operation starts long before any machine is bolted down. Walk the floor during a shift change and watch how operators move between unwinds, folders, and poly wrappers. You'll spot mismatches that a line-balancing spreadsheet never shows, like a folder that outpaces its downstream stacker, forcing someone to clear a pile-up every twenty minutes. Drift out of spec rarely comes from one dramatic failure; it hides in worn folding plates, uneven unwind tension, and vacuum belts that lose grip after a few hours. Instead of chasing the rated speed from the brochure, match folder output to what your packaging and case packing stations can actually sustain, then leave a small buffer for bad rolls and late-arriving pallets. Running slower but steadier almost always beats running fast in bursts.
Changeovers and daily upkeep tell you more about line health than any startup checklist. The tiny things eat entire shifts: a missing adjustment wrench, unmarked guide rail positions, or a spare knife stored three aisles away. Standardize those details once and they stop stealing time. Maintenance logs usually reveal patterns before a full stop. Repeated tweaks to the same bearing housing, creeping motor amp draws, or lubrication intervals that slowly stretch out are early warnings worth acting on. Finally, build the layout so a new operator or a transferred worker can step in without asking a veteran. Use color-coded paths, photos at each station, and part designs that only fit one way. That kind of visual clarity keeps the line reliable even when your best people move on, and it makes training a matter of hours rather than weeks.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/