Powder Valve Solutions: The Ultimate Guide to Effective Flow Control
2026-10-09
Getting powder to flow exactly when and where you need it is a challenge that quietly shapes industries—from food processing to pharmaceuticals. One wrong valve choice can mean clogging, dust leakage, or inconsistent batches. This guide to powder valve solutions cuts through the noise, focusing on how the right flow control turns a stubborn material into a predictable process. You’ll discover practical selection criteria, common failure points, and why AVM has become a go-to name for engineers who refuse to compromise on precision.
How Valve Geometry Shapes Powder Flow Patterns
Valve internals rarely get credit for how they steer bulk solids, yet their contours do more than open and close a line. A flat disc in a butterfly valve, for instance, creates a sharp-edged obstruction that can split a powder stream unevenly, leaving fines to slip past the edges while coarser particles pile up behind the plate. This mismatch often leads to localized velocity gradients, which in turn encourage segregation even before the material reaches the next process step.
By contrast, a full-bore ball valve or a carefully profiled rotary valve tends to preserve the cross-sectional area more consistently, letting the powder maintain a more uniform front as it moves through. The rounded passage reduces the abrupt changes in direction that cause shear planes to form within the bed—planes where particles of different sizes drift apart. In practice, this means a valve with a smooth, gradual transition from inlet to outlet can keep a blend homogeneous far better than one with sharp corners or sudden expansions.
There is also the matter of dead zones. Pocketed areas behind a partially closed gate or around the stem of a globe valve can trap material, allowing it to compact or absorb moisture over time. When that stagnant powder finally breaks loose, it enters the main flow as a slug with altered density and moisture content, disrupting what was otherwise a steady stream. The shape of the valve, then, is not just a mechanical afterthought—it actively dictates whether the powder moves as a coherent mass or fractures into unpredictable patterns.
Choosing Between Rotary, Butterfly, and Slide Gate Designs
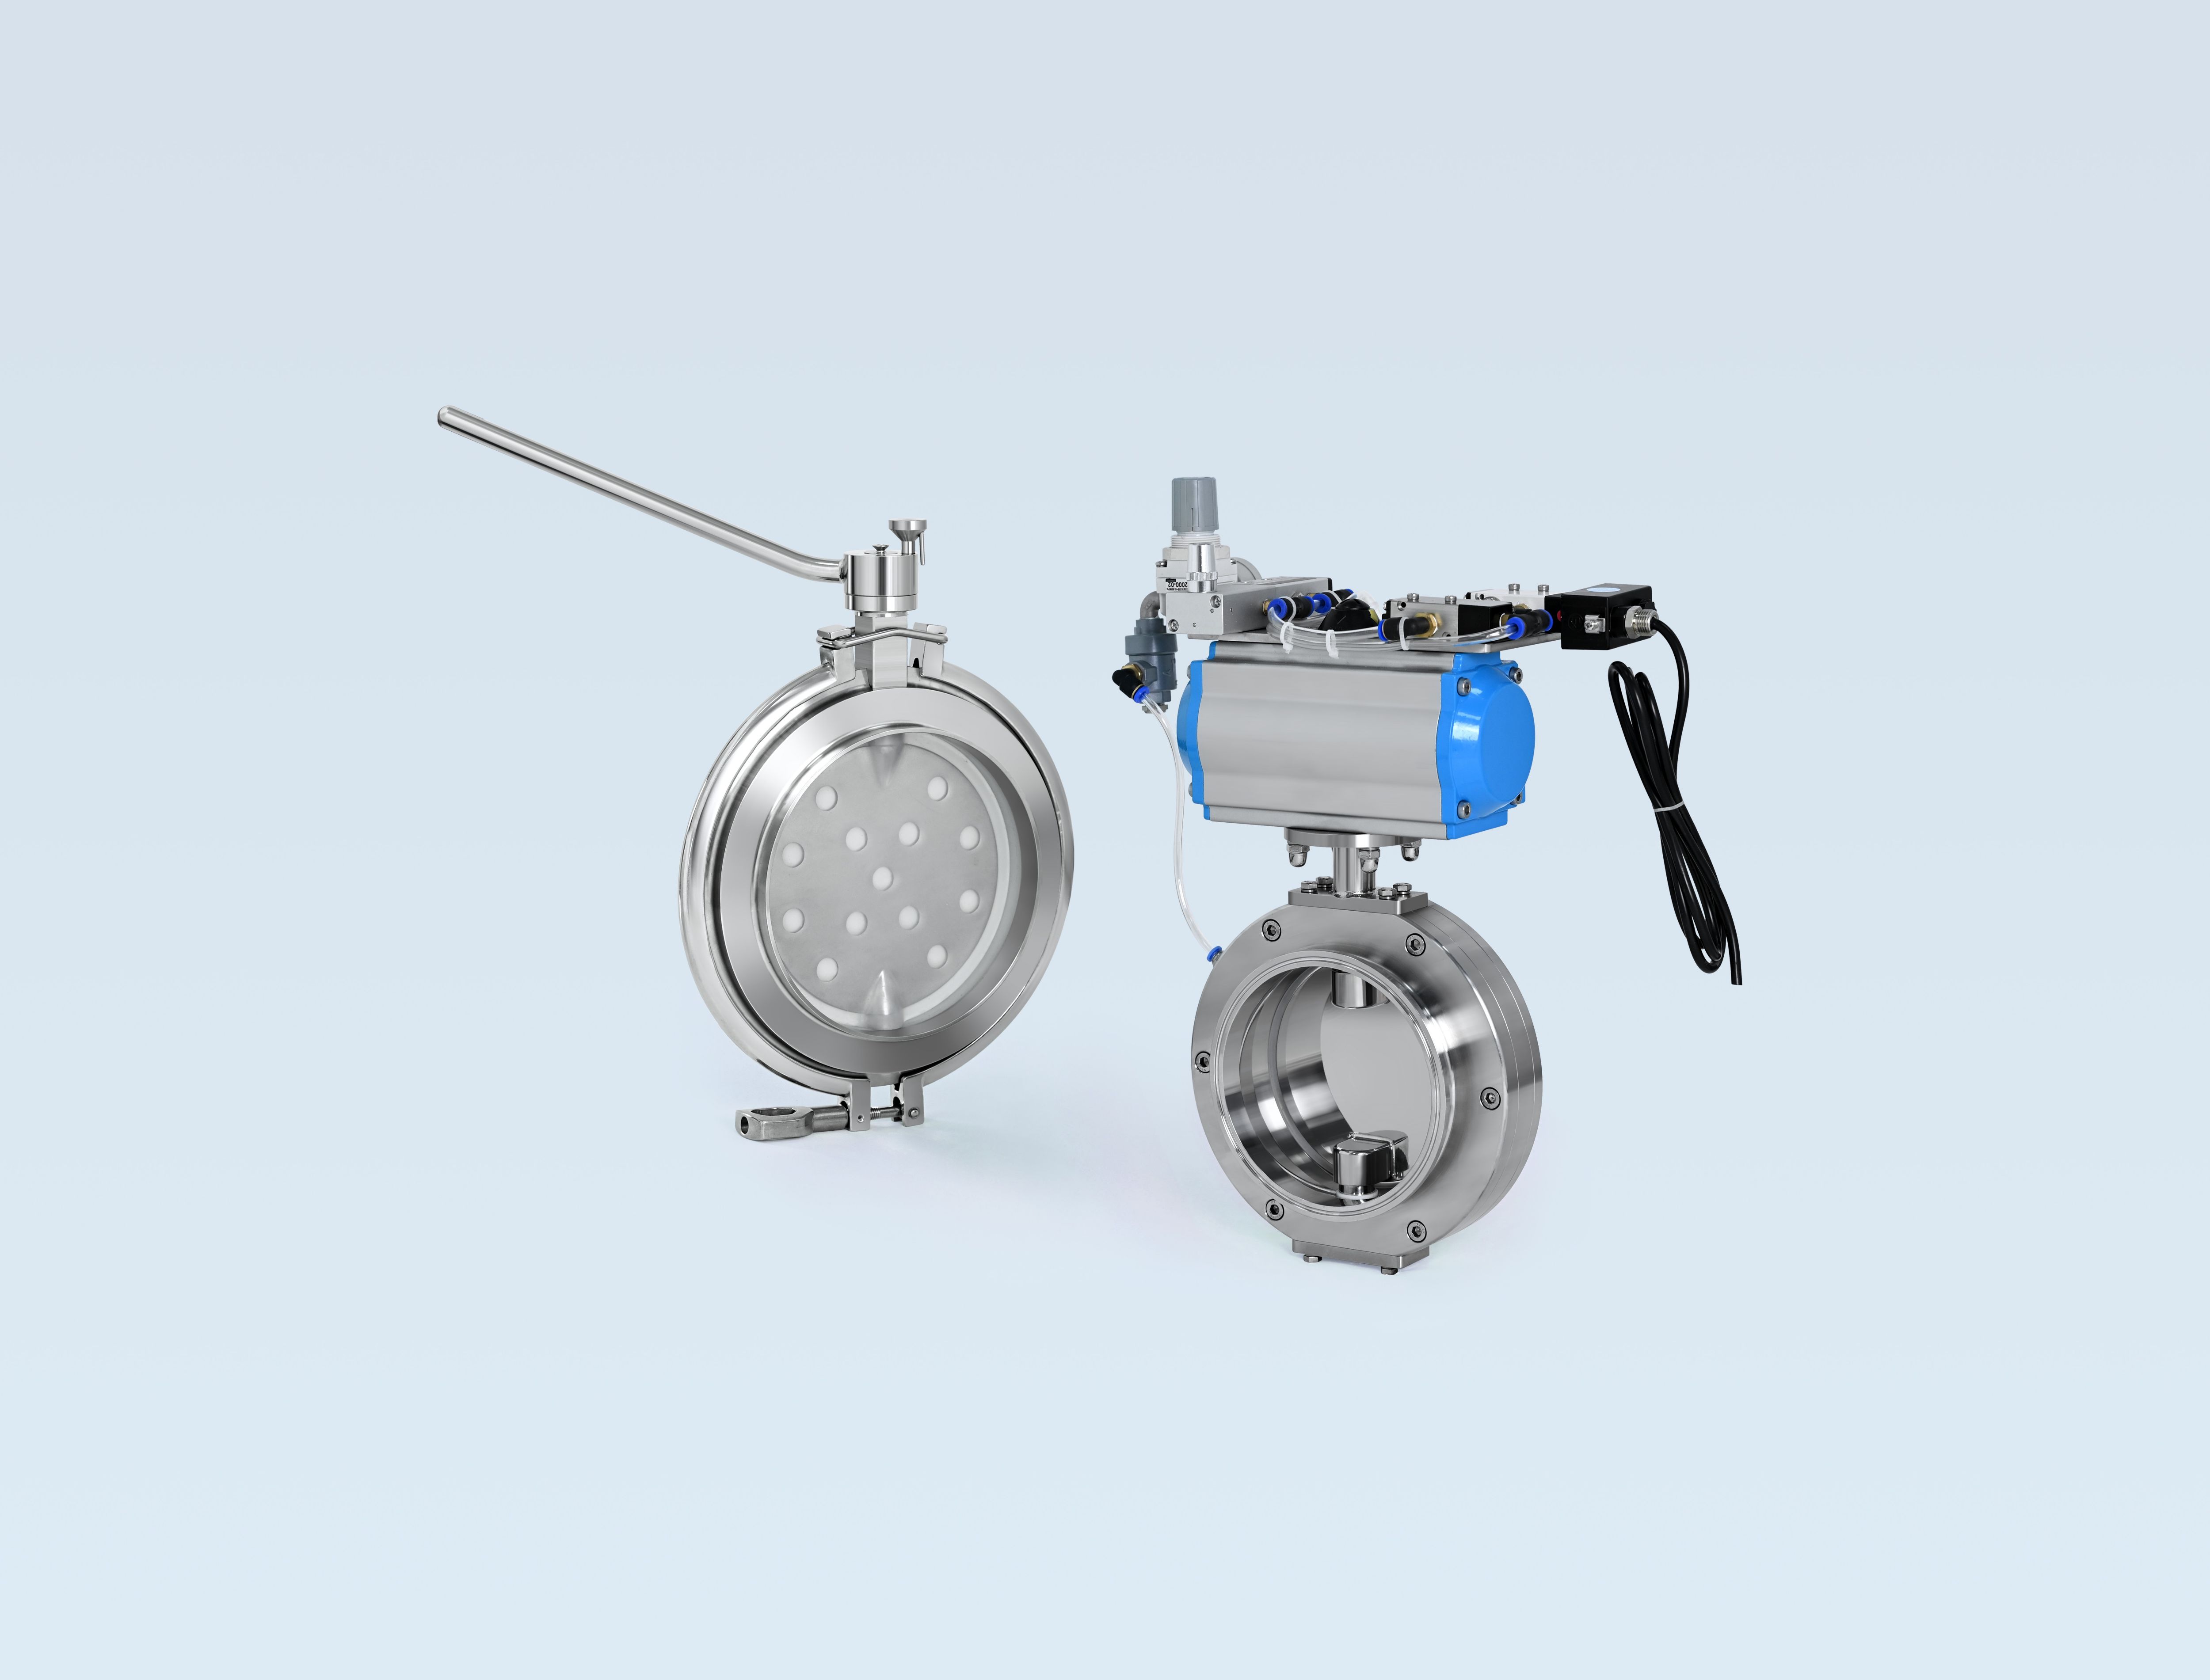
Rotary gate systems tend to work best when you're dealing with high-traffic areas that still demand a controlled flow. Their circular motion creates a natural rhythm for pedestrians, and the enclosed structure prevents people from slipping past the edges. But they take up more room than you might expect, so cramped entrances often rule them out early.
Butterfly gates shine in tight spots. The two folding panels collapse into a surprisingly compact footprint, which makes them a favorite for subway turnstiles and office lobbies where every inch counts. They're also quicker to cycle than rotary units, though the gap between the closed panels can be a weak point if you're worried about tailgating.
Slide gate designs prioritize sheer width and smooth operation. Instead of rotating or folding, the panel glides sideways into a pocket or along a rail, which means you can open up a passage that feels almost barrier-free when it's retracted. They demand more maintenance for the track system, and dirt or debris can cause jams, but for wheelchair access or moving bulky equipment, nothing beats a slide gate's clear opening.
Sealing Strategies for Fine and Sticky Powders
Fine and sticky powders have a way of finding every tiny gap. The first move is usually to ditch rigid metal-to-metal seals and go with an inflatable gasket that stays relaxed during filling and only tightens when the vessel closes. A light air sweep around the seal face helps stop dust from packing into the crevice before it hardens.
Titanium dioxide, starch, and similar materials tend to smear rather than flow. That means the sealing surface must let go of the powder instead of holding onto it. Food-grade silicone or PTFE lip seals with a polished contact zone work better here because they shed buildup more easily. Adding a simple labyrinth shield in front of the main seal catches most of the fines before they ever reach the critical gap.
At discharge points, a double-flap valve or a rotary airlock with spring-loaded blades gives you more control than a standard butterfly valve. The key is to keep the speed low so the powder doesn't get pressed into the seal under high force. A carbide or polymer coating on the sealing area plus short reverse air pulses between cycles removes the residual layer that would otherwise cause leaks after a few batches.
Air-Assisted Discharge: When and Why It Works
Air-assisted discharge becomes relevant when gravity alone cannot move material out of a bin or silo, especially with cohesive powders or irregularly shaped particles that tend to bridge or rat-hole. The key is not simply adding air, but introducing it at the right point—usually near the discharge outlet or along the hopper walls—to reduce interparticle friction and break stable arches. This method works because the air creates a local fluidization effect, reducing the bulk density around the outlet and allowing material to flow more freely without the need for mechanical vibration or manual intervention.
In practice, the success of air-assisted discharge depends heavily on matching the air pressure and flow rate to the material's permeability and moisture content. Too little air won't overcome cohesive forces, while too much can cause channeling or blow holes that bypass the remaining material. Operators often find that intermittent pulses are more effective than continuous flow, as each pulse disrupts the particle network and lets gravity take over. This approach is particularly useful for materials like wet sand, filter cake, or fine ores, where traditional flow aids either fail or create excessive dust.
Another reason air-assisted discharge works where other methods struggle is that it can be installed with minimal structural modification. Instead of adding liners or changing bin geometry, a series of air pads or nozzles can be retrofitted to an existing vessel. The maintenance is also lower because there are no moving parts inside the material stream. That combination of low intervention, adjustable parameters, and immediate effect makes it a practical solution for processors who need to restore flow without shutting down for extended periods.
Preventing Segregation with the Right Valve Placement
Segregation in storage vessels rarely starts at the valve itself, but the discharge point exerts a powerful influence on how the entire bed moves. When a valve is positioned off-center or too close to a hopper wall, it can encourage funnel flow, where a narrow channel forms above the outlet while surrounding material remains static. That static material is precisely where fines and coarse particles separate, creating quality problems later. By shifting the valve to the center of a properly designed hopper outlet and ensuring the opening is large enough, you help the whole cross-section move downward together. This mass flow pattern draws material from all regions of the bin, so a representative blend reaches the downstream process rather than a segregated fraction.
Multi-outlet arrangements need even more care. If one valve opens faster than others or if the spacing between discharge points is uneven, the resulting flow paths can distort and create dead zones between active channels. A better approach is to treat valve placement as part of the hopper geometry, not an afterthought. Match the valve size and location to the hopper angle and outlet dimensions, and consider using insert designs or flow-assist devices only after the primary placement is correct. Small adjustments in valve symmetry and elevation can mean the difference between a bin that self-blends and one that continuously unloads segregated material.
From Manual to Fully Automated Powder Handling
Powder handling has long been a bottleneck in production lines where operators once scooped, weighed, and transferred materials by hand. Every manual step introduced variability—spills, inconsistent dosing, and exposure risks—while slowing throughput. Early attempts to improve relied on semi-automatic feeders and local controls, but these still demanded constant oversight and frequent recalibration.
The shift toward fully automated powder handling changes the operational equation. Closed systems now convey, meter, and discharge powders with minimal human touch, using loss-in-weight feeders, vacuum conveying, and recipe-driven controls. This removes guesswork from batch consistency and lets a single operator supervise multiple lines instead of tending a single hopper.
What makes the transition practical is modular automation. Rather than replacing an entire plant, teams can retrofit existing equipment with smart sensors and central software that log every gram moved. The result is traceable, repeatable handling that cuts waste, protects workers from dust, and frees skilled staff for tasks that actually benefit from human judgment.
FAQ
Powder valves are engineered to handle dry bulk solids, which behave nothing like liquids or gases. They often include features like inflatable seals, wider clearances, and abrasion-resistant liners to prevent jamming, dust leakage, and wear from fine particles.
For cohesive powders, butterfly valves with special disc profiles or rotary airlocks can work, but pinch valves and dome valves often shine because their full-bore opening and closing action reduces dead zones where material can accumulate and harden.
Use valves with proper shaft sealing, such as double lip seals or purged packing glands, and consider a vent port if the powder is aerated. Secondary seals or containment shrouds also help when handling toxic or very fine dusts.
Abrasive powders like silica or alumina will quickly erode soft metals and elastomers. Hardened steel, ceramic-coated internals, or replaceable wear liners can dramatically extend service life, though they cost more upfront.
Pneumatic actuators are common because they provide quick, reliable operation and can be made intrinsically safe for dusty environments. Electric actuators offer more precise positioning and feedback, but they need proper enclosures to avoid dust ignition risks.
It depends on the duty cycle and powder abrasiveness, but a good rule is to inspect seals, bearings, and liners every 1,000 to 5,000 cycles or at least quarterly. Listen for air leaks on pneumatic systems and check for buildup around the seat area.
Usually not optimally. Free-flowing powders need tight shutoff to prevent dribbling, while cohesive powders need a more aggressive opening action to break bridges. You can achieve both with a specially designed dome valve or a rotary valve with adjustable tip clearance, but often two valve types are better.
Dust explosion risk is the big one. Valves should be grounded, use antistatic materials, and avoid metal-to-metal sparks. For combustible powders, look for ATEX or NFPA compliance, and consider flame arrestors or isolation valves in connected ductwork.
Conclusion
Effective powder flow control depends first on how valve geometry interacts with the material’s bulk behavior. A sharply tapered opening, for instance, encourages mass flow but can crush friable particles, while a wider, more gradual transition suits cohesive or sticky powders better. Rotary valves offer precise metering and suit free-flowing granules, butterfly designs provide compact shutoff for moderate duties, and slide gates handle coarse, abrasive media with fewer jamming risks. Matching the valve type to the powder’s angle of repose, particle size, and moisture content eliminates many downstream headaches.
Sealing fine or sticky powders calls for careful choices: inflatable seals, purge ports, and polished contact surfaces reduce build-up and leakage. Air-assisted discharge using fluidizing pads or aeration nozzles works well when powders bridge or rat-hole, but only if the air is directed near the valve outlet and not allowed to disturb the powder bed excessively. Valve placement also matters—positioning the valve at the base of a properly designed hopper, rather than halfway down a chute, helps prevent segregation by maintaining a consistent velocity profile. Finally, shifting from manual operation to fully automated powder handling improves repeatability, but automation alone cannot fix a poorly selected valve; the underlying flow characteristics must guide the upgrade.
Contact Us
Contact Person: Ananda
Email: [email protected]
Tel/WhatsApp: 8619016718200
Website: https://www.wzaomi.com