Best Sewer Pipe Cleaning Machine Factory Traits That Signal Quality
2026-10-09
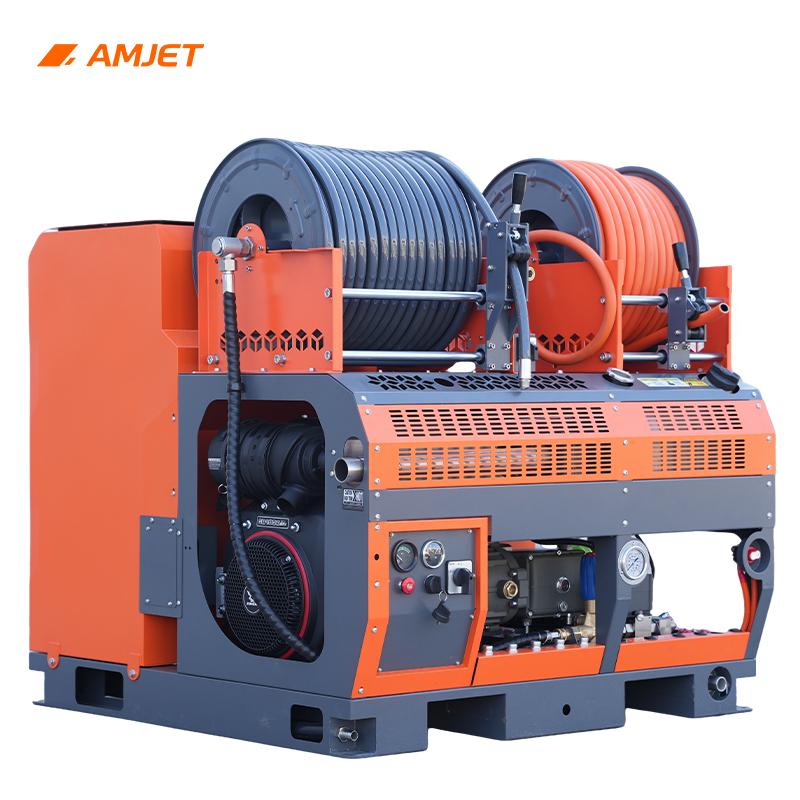
When every supplier claims their sewer pipe cleaning machines are built to last, how do you separate real manufacturing quality from clever marketing? The answer often hides in factory traits that are easy to overlook—raw material handling, weld consistency, pressure testing, and assembly discipline. In this post, we unpack the signals that separate dependable equipment from costly downtime. As you evaluate potential partners, keep brands like AMJET in mind, because a factory that openly demonstrates these traits is already ahead of the pack.
Raw Material Traceability You Can Actually Confirm
Every incoming lot gets a unique batch code that stays with it from receiving through cutting and assembly. That code links to a live log showing supplier name, mill location, production date, and the certificate of analysis for that specific shipment—not a generic PDF borrowed from a catalog.
At any point, a buyer can enter the lot number into our portal and pull up the actual inspection notes, including any hold or rejection events that happened before the material was approved. There is no polished summary hiding a failed first test; the record shows exactly what was flagged, what was corrected, and who signed off on the final release.
For fibers and leathers sourced from smaller producers, we attach field-level documentation such as harvest coordinates, processing date, and transport timestamps. Discrepancies between the supplier's claim and the physical shipment are noted in the same record, so confirmation does not depend on taking our word for it.
In-House Load Testing That Mimics Real Blockages
Instead of relying on narrow lab conditions, our test rig is built around the exact failure patterns we see in field reports. We collect pulled debris, take measurements, and recreate the same mass, density, and snag points inside clear pipe sections. That means a partial grease clog or a mat of wet wipes isn’t approximated with a simple rubber ball or a pressure gauge—it’s built layer by layer until it behaves like the real thing.
Each run is filmed from multiple angles and instrumented at several points along the line, so we can see not just when a tool clears the blockage, but how the material shifts, breaks apart, or packs tighter under load. We also vary the scenario: aged cast iron with scale, PVC with a bellied section, or a long sweep with a root intrusion mock-up. These aren’t pass/fail stunts; they’re repeated cycles that expose wear on cutting heads, torque limits on cables, and weak spots in seals before a single unit ships.
The result is a load test that reads more like a worst-case service call than a controlled demo. When a machine leaves our floor, it has already faced the kind of stubborn, mixed-material blockages that cause callbacks in the field. That’s the standard we hold, and it’s why our posted specs tend to be conservative rather than inflated.
Frame Welds and the Art of Not Overbuilding
A welded frame doesn’t need to look like it was built to survive a bomb blast. The real skill lies in knowing exactly where strength is required and where extra material only adds weight without purpose. Good welders read the load paths, understand how stress flows through tubes, and place their beads accordingly. It’s not about laying down the biggest, fattest weld possible—it’s about making each pass count, keeping the heat affected zone tight, and letting the tube’s natural properties do their job.
Overbuilding often comes from fear or habit. Someone adds a gusset here, a thicker wall there, thinking it makes the frame safer. But in reality, a frame that’s too stiff can ride harshly, transfer more vibration, and even crack at the edges of those overbuilt reinforcements. The art of not overbuilding means trusting your design, using proper joint preparation, and selecting tube diameters and wall thicknesses that match the expected loads. A clean, consistent weld with full penetration on a well-fitted joint will outperform a messy stack of extra metal every time.
At the end of the day, the goal is a frame that feels alive under the rider—strong where it must be, light where it can be, and free of unnecessary clutter. That kind of balance comes from experience, not just from following a blueprint. It’s the difference between a frame that merely holds together and one that dances down the trail with confidence.
Motor and Pump Matching Without Sales Hype
Matching a motor to a pump starts with torque, not horsepower. Look at the pump's required torque at its operating speed, then confirm the motor can deliver that torque continuously without exceeding its rated temperature rise. Oversizing a motor wastes energy and increases cost; undersizing leads to premature winding failures. The nameplate kW rating is a rough guide, but the real work happens at the shaft.
Pay attention to the pump's speed-torque curve during startup. Centrifugal pumps often start with low torque, while positive displacement pumps may need high starting torque against a closed valve. A motor that starts across-the-line draws high current, so verify the supply can handle the inrush without excessive voltage drop. If not, a soft starter or variable frequency drive makes sense, but only if the application actually benefits—don't add electronics just to feel modern.
Ambient conditions matter more than most catalogues admit. A motor rated for 40°C at sea level will lose life in a hot, humid pump room. Check insulation class, service factor, and enclosure type against the real environment. And remember: a perfectly matched set still needs proper alignment and a solid base. No amount of clever matching overcomes a misaligned coupling eating bearings every few months.
How the Factory Handles Prototypes and Small Runs
The factory treats prototypes and small runs not as interruptions, but as a natural part of the production cycle. Instead of forcing every job into full-scale manufacturing, the team maintains dedicated workstations and a small crew that can switch between low-volume tasks and high-volume orders without losing rhythm. This flexibility means a prototype can move from CAD file to first article in a matter of days, not weeks.
For small runs, the approach is deliberately lean. Material ordering is handled in precise batches, and setup times are trimmed by using modular fixtures that stay ready near each machine. Since the same operators who handle large orders also work on small batches, there is no learning curve penalty. That consistency shows up in the final parts: a 50-piece run gets the same dimensional checks and surface finish as a 50,000-piece order.
One practical benefit is that design changes can be tested without betting on a huge inventory. If a prototype reveals a weak spot or an awkward assembly step, the factory can adjust tooling and run another short batch almost immediately. This back-and-forth happens on the floor, with engineers and machinists standing at the same bench rather than trading emails for a week. The result is a smoother handoff from prototype to production, and fewer surprises when volumes finally ramp up.
Spare Parts Availability as a Quality Signal
A product's lifespan rarely ends with the initial purchase. The ease with which you can find a replacement motor, a specific gasket, or even a proprietary screw says a great deal about what the manufacturer thinks of its own creation. When spare parts are readily available years after a model is discontinued, it quietly signals that the company anticipated long-term use rather than planned obsolescence. Buyers pick up on this without always articulating it: a brand that stocks parts for a decade-old appliance is essentially promising that the original build quality was worth supporting.
From the manufacturer's side, maintaining a spare parts inventory is far from cheap. It ties up warehouse space, requires forecasting demand for obscure components, and forces design teams to avoid unnecessary part proliferation. A company that commits to this overhead is betting that its reputation for durability will justify the expense. Compare that to a brand that treats every product as a one-off transaction, where a broken plastic clip means tossing the entire unit. The difference in spare parts strategy is a direct reflection of how much faith the producer has in its own engineering.
This signal becomes even more valuable in secondhand markets and professional settings. A used car model known for affordable, easily sourced parts holds its resale value better than one that forces owners to scour junkyards or pay for custom fabrication. Similarly, a contractor choosing between two power tool brands will lean toward the one whose brushes, switches, and bearings can be ordered without a six-week wait. In these contexts, spare parts availability acts as a proxy for the manufacturer's overall quality commitment, often influencing purchasing decisions long before any formal warranty language is read.
FAQ
Walk the production area and check whether welding stations use jigs and fixtures rather than freehand assembly. A clean, organized floor with calibrated torque tools and material traceability tags usually means the factory controls variance. If you see rusted raw stock sitting next to finished components or unlabeled cable reels, treat that as a warning sign.
High-quality factories tend to specify drum and frame steel with documented yield strength instead of generic mild steel. They also avoid mixing suppliers for critical wear parts like chains, nozzles, and hoses. Ask for mill certificates or batch numbers; if the factory cannot produce them quickly, they probably have not been tracking inputs.
A factory that pressure-tests every pump and hose reel before crating will catch leaks that would otherwise surface on a job site. Look for a dedicated test bay with water recovery and load simulation, not just a quick spin of the drum. Factories that skip this step usually push warranty risk onto the buyer.
Look beyond the standard one-year promise. A factory that offers extended coverage on gearboxes, pumps, and frames—and keeps spare parts on the shelf for older models—is signaling confidence. Responsive technical support with real troubleshooting, not scripted replies, also tells you they understand how contractors actually use the equipment.
Ask for a non-standard drum capacity, a different engine mount, or a trailer package with specific axle ratings. A capable factory will come back with drawings, load calculations, and a timeline. If they simply say yes to everything without questioning feasibility, they may be selling catalog copies rather than engineered solutions.
Factories that openly name their pump, engine, and hydraulic suppliers—and allow third-party inspection—tend to have fewer hidden substitutions. Watch for vague answers or sudden changes in brand when you request a quote. Consistent sourcing protects you from machines that look identical but perform differently six months later.
Check powder coating thickness on frames, sealed electrical connectors, and whether hose reels spin without wobble. Small things like properly grommeted wiring and rust-proof fasteners show the factory applies the same care to areas buyers rarely inspect. Sloppy finishing often mirrors sloppy internal processes.
Conclusion
When evaluating a sewer pipe cleaning machine factory, the first thing worth checking is whether they can actually prove where their raw materials come from. A quality factory doesn't hide behind vague sourcing claims; they show you mill certificates and batch numbers that you can cross-reference. This traceability extends beyond steel to every hose, coupling, and seal. If they can't walk you through the supply chain without hesitation, that's a red flag. Equally telling is how they test finished machines. The best factories don't just run pumps dry on a bench—they build test rigs that mimic real blockages, including grease plugs, root intrusions, and collapsed pipe sections. Watching a machine chew through a deliberately packed test line tells you more than any brochure ever will.
Another overlooked quality signal is the frame. Some factories overbuild with thick, ugly welds that add weight without adding durability; others underbuild and the machine twists under load. The sweet spot is a frame that's engineered with finite element analysis and welded by people who understand fatigue cycles, not just filler metal. The same logic applies to motor and pump matching. A reputable factory will show you pump curves and motor torque charts side by side, no sales hype, just math. They should also be willing to handle prototypes or small runs without treating you like an inconvenience, because that flexibility often reflects a deeper engineering culture. Finally, ask about spare parts availability. If the factory stocks common wear items and can ship a replacement hose reel or nozzle within days—not months—that's a quiet proof of long-term quality thinking.
Contact Us
Contact Person: Mike
Email: [email protected]
Tel/WhatsApp: +86 19545555505
Website: https://www.amjeting.com/